Use 3D Printed Rocket Engines: The Future of Space Propulsion as a Practical Choice
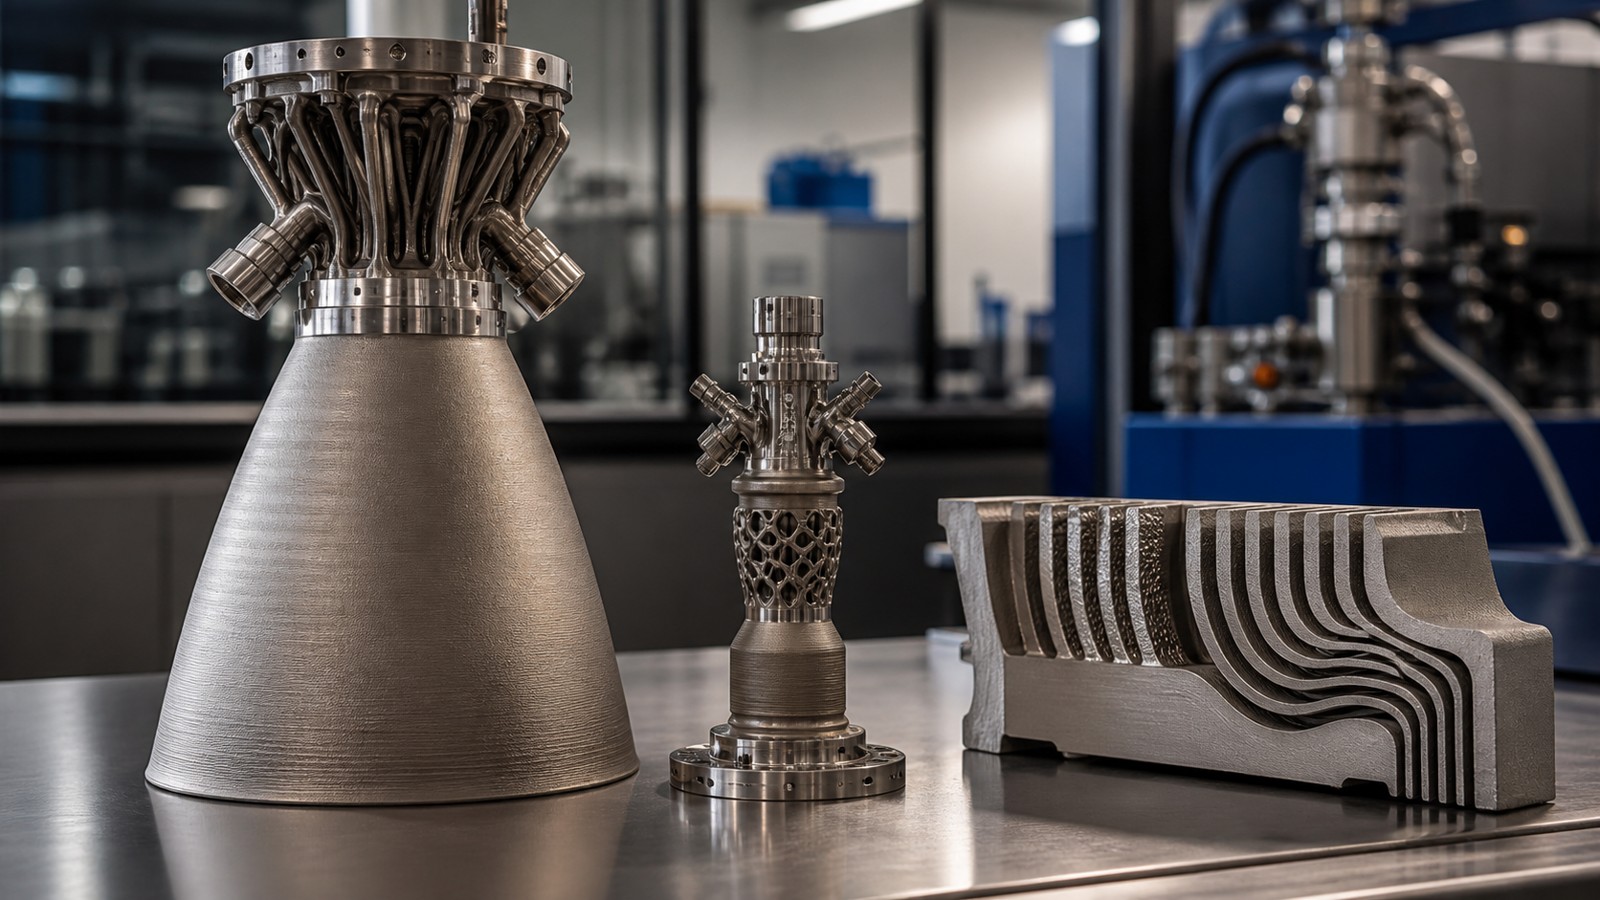
3D Printed Rocket Engines: The Future of Space Propulsion can sound broad, but the real decision usually shows up in one stubborn feature of the part. This guide is written for readers curious about why engine parts benefit from additive manufacturing, so it keeps the explanation close to examples such as manifold rings, injector plates, and regenerative cooling channels. The important questions are concrete: how alloy selection changes the setup, where test repeatability creates risk, and what evidence proves that the chosen approach actually improved the print. Instead of treating the topic as a list of isolated tips, the article follows the way a maker or small shop would think through a real job: choose a direction, test the most fragile assumption, read the result honestly, and only then commit to a larger or more expensive build. It also separates this title from nearby September topics by focusing on propulsion hardware, using nozzle sections and chamber liners as working examples instead of repeating the same material checklist.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose visible layer lines, fragile details, support scars, and oversized assemblies before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful sanding, filling, priming, painting, sealing, and display mounting.
A: It is most useful for makers building display pieces, props, miniatures, and gifts.
The Practical Job Behind Printed Rocket Engines Future
The first change is usually not dramatic. With 3D Printed Rocket Engines: The Future of Space Propulsion, the earliest difference often appears in alloy selection, because that choice decides whether the print is being asked to do something realistic. A maker looking at manifold rings should not judge success only by whether the part finished; the better question is whether the printed shape supports its real job. That is why propulsion hardware matters: it turns a vague preference into a checkable decision. For printed rocket engines future, check test stands.
The same topic can look very different on injector plates. A decorative version may tolerate a soft corner or a longer cleanup pass, while a functional version may fail if a hole shifts, a tab flexes, or a mating face needs sanding. Readers get better results when they name that difference before slicing the model. Useful evidence: alloy selection on manifold rings.
For test stands, the most useful detail is not whether the print completed, but whether inspection route made the part easier to trust after handling. That distinction keeps the article focused on evidence rather than enthusiasm. That gives printed rocket engines future its own checkpoint.
A shop using 3D Printed Rocket Engines: The Future of Space Propulsion could test the riskiest corner, hinge, channel, or mating face on nozzle sections. If that small piece answers the question, the full model becomes a confirmation instead of a gamble. Use regenerative cooling channels before the larger print.
Setup Choices That Shape the Outcome
The decision gets real when test repeatability meets the limits of the printer and material. This is where generic advice starts to thin out, because a setting that helps regenerative cooling channels may make nozzle sections worse. The print should be judged against its role: display piece, fit check, shop aid, customer prototype, classroom demo, or end-use component. Useful evidence: test repeatability on manifold rings.
A useful reader perspective is to ask what failure would be most expensive. Sometimes it is wasted filament; sometimes it is a missed delivery, a brittle hinge, a support scar in the worst possible spot, or a part that looks fine until it is assembled. That risk should guide the first test more than a popular profile found online. That gives printed rocket engines future its own checkpoint.
For close comparison titles, this section is especially important. The goal is not to crown a universal winner. It is to separate the job where one option is comfortable from the job where the other option is worth the extra tuning. Use regenerative cooling channels before the larger print.
The practical standard changes with the audience. A classroom sample can teach the concept with visible layer lines, while a customer prototype needs cleaner fit and a more predictable finish. 3D Printed Rocket Engines: The Future of Space Propulsion should be judged against that standard from the beginning. For printed rocket engines future, check nozzle sections.
That is why test repeatability deserves a separate note. It may seem like a small setup choice, but it often decides whether the part can be repeated without rediscovering the same problem. Useful evidence: inspection route on chamber liners.
Small Evidence Before Big Commitments
Before a full print, isolate the feature that carries the most uncertainty. For 3D Printed Rocket Engines: The Future of Space Propulsion, that might mean a corner of chamber liners, a small section of test stands, or a short coupon that reveals thermal stress without consuming the whole afternoon. A focused test is not a delay; it is a way to make the next decision cleaner. That gives printed rocket engines future its own checkpoint.
The test should be small enough to repeat but realistic enough to matter. A flat rectangle may prove bed adhesion, but it will not reveal how a thin upright wall, a trapped support, or a snap feature behaves. The best test includes one problem that the final part must solve. Use regenerative cooling channels before the larger print.
Cost also has to include attention. A material or method that demands drying, enclosure control, careful supports, or post-processing may still be the right choice, but only when the part’s value justifies those extra decisions. For printed rocket engines future, check nozzle sections.
In a small batch, one failed assumption can repeat across every copy. Testing nozzle sections before the batch protects time, material, and confidence without turning the project into a long research project. Useful evidence: alloy selection on chamber liners.
Comparing Prints Without Guesswork
Reading the first result takes more discipline than printing it. Look at the part after it cools, after supports come off, after washing or sanding if those steps apply, and after it touches the object it must fit. That second look often reveals whether channel complexity is merely acceptable or genuinely under control. Use regenerative cooling channels before the larger print.
Good notes do not need to be long. Record the material condition, orientation, key setting change, cleanup effort, and the one thing the next version should improve. If the note cannot explain why the next print will be different, it is probably just a diary entry rather than useful evidence. For printed rocket engines future, check nozzle sections.
The comparison should include handling. A print that looks crisp on the plate can still feel wrong when it bends, clips, slides, warms up, or carries a load. That is where 3D Printed Rocket Engines: The Future of Space Propulsion becomes a practical judgment instead of a search-result summary. Useful evidence: test repeatability on chamber liners.
Many readers improve faster when they keep the final use visible. A part that will be painted, assembled, warmed, flexed, or washed needs to be checked after that step, not only while it looks fresh on the build plate. That gives printed rocket engines future its own checkpoint.
If inspection route is the weak point, the next print should target that weakness directly. A beautiful unrelated surface cannot compensate for a feature that fails where the part actually works. Use manifold rings before the larger print.
When the Material or Method Earns Its Place
Every option has a tradeoff, and the useful ones should be named before the print begins. Better detail can mean slower production. More heat resistance can mean more warping control. A cleaner support strategy can increase print time. A stronger part can be harder on the nozzle or less forgiving during assembly. For printed rocket engines future, check nozzle sections.
For readers curious about why engine parts benefit from additive manufacturing, the best choice is usually the one that removes the most important risk without adding two new problems. That might favor a simple material for manifold rings and a more demanding setup for nozzle sections. The answer should follow the part, not the label on the spool or bottle. Useful evidence: thermal stress on chamber liners.
For nozzle sections, the most useful detail is not whether the print completed, but whether channel complexity made the part easier to trust after handling. That distinction keeps the article focused on evidence rather than enthusiasm. That gives printed rocket engines future its own checkpoint.
A shop using 3D Printed Rocket Engines: The Future of Space Propulsion could test the riskiest corner, hinge, channel, or mating face on injector plates. If that small piece answers the question, the full model becomes a confirmation instead of a gamble. Use manifold rings before the larger print.
Troubleshooting Without Chasing Noise
The common mistake is changing too many variables at once. If part consolidation is poor, the fix might be temperature, drying, orientation, support interface, speed, or model geometry. Changing all of them can produce a better-looking part while teaching nothing about why it improved. Useful evidence: channel complexity on chamber liners.
Another mistake is trusting the first decent print. A single success is useful, but it does not prove repeatability. Print a second small sample, assemble the mating feature, or compare the same geometry in a slightly different orientation before assuming the method is settled. That gives printed rocket engines future its own checkpoint.
Beginners also undercount cleanup. Supports, sanding, curing, drying, trimming, or insert installation can matter as much as print time. If cleanup is the hidden bottleneck, the technically stronger option may not be the better workflow. Use manifold rings before the larger print.
The practical standard changes with the audience. A classroom sample can teach the concept with visible layer lines, while a customer prototype needs cleaner fit and a more predictable finish. 3D Printed Rocket Engines: The Future of Space Propulsion should be judged against that standard from the beginning. For printed rocket engines future, check injector plates.
That is why inspection route deserves a separate note. It may seem like a small setup choice, but it often decides whether the part can be repeated without rediscovering the same problem. Useful evidence: test repeatability on regenerative cooling channels.
Finish With One Clear Test
The next print should answer one question that the article made visible. It might test inspection route, compare two orientations, try a smaller support interface, dry one spool, or print the same feature in a different material. Keep the test narrow enough that the result is not ambiguous. That gives printed rocket engines future its own checkpoint.
After that, the project can scale with more confidence. Move from a coupon to injector plates, from a fit corner to the full assembly, or from a single material trial to a short production run. That progression keeps 3D Printed Rocket Engines: The Future of Space Propulsion grounded in evidence and gives the reader a useful way to act today. Use manifold rings before the larger print.
Cost also has to include attention. A material or method that demands drying, enclosure control, careful supports, or post-processing may still be the right choice, but only when the part’s value justifies those extra decisions. For printed rocket engines future, check injector plates.
In a small batch, one failed assumption can repeat across every copy. Testing injector plates before the batch protects time, material, and confidence without turning the project into a long research project. Useful evidence: thermal stress on regenerative cooling channels.