SLS Cost Is More Than Machine Time
SLS pricing depends on machine time, powder use, packing density, cooling time, labor, depowdering, finishing, rejects, and overhead. The process can be economical for batches of complex nylon parts, but it is rarely the cheapest way to make one simple object.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose slow throughput, inconsistent tolerances, weak parts, and unclear requirements before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful inspection, part testing, finishing, assembly, and revision control.
A: It is most useful for teams using 3D printing as a workflow tool, not only a hobby machine.
SLS Cost Is More Than Machine Time
SLS pricing depends on machine time, powder use, packing density, cooling time, labor, depowdering, finishing, rejects, and overhead. The process can be economical for batches of complex nylon parts, but it is rarely the cheapest way to make one simple object.
For businesses, cost per usable part matters more than cost per build. A full build with good nesting may spread setup and cooldown across many parts. A half-empty build may make each part expensive even when the geometry is small.
The Main Cost Drivers
The largest drivers are part volume, bounding box, build height, material type, surface finish, and required tolerance. Tall parts can increase build time because the machine must spread and fuse more layers. Bulky solid parts consume more powder and may trap heat.
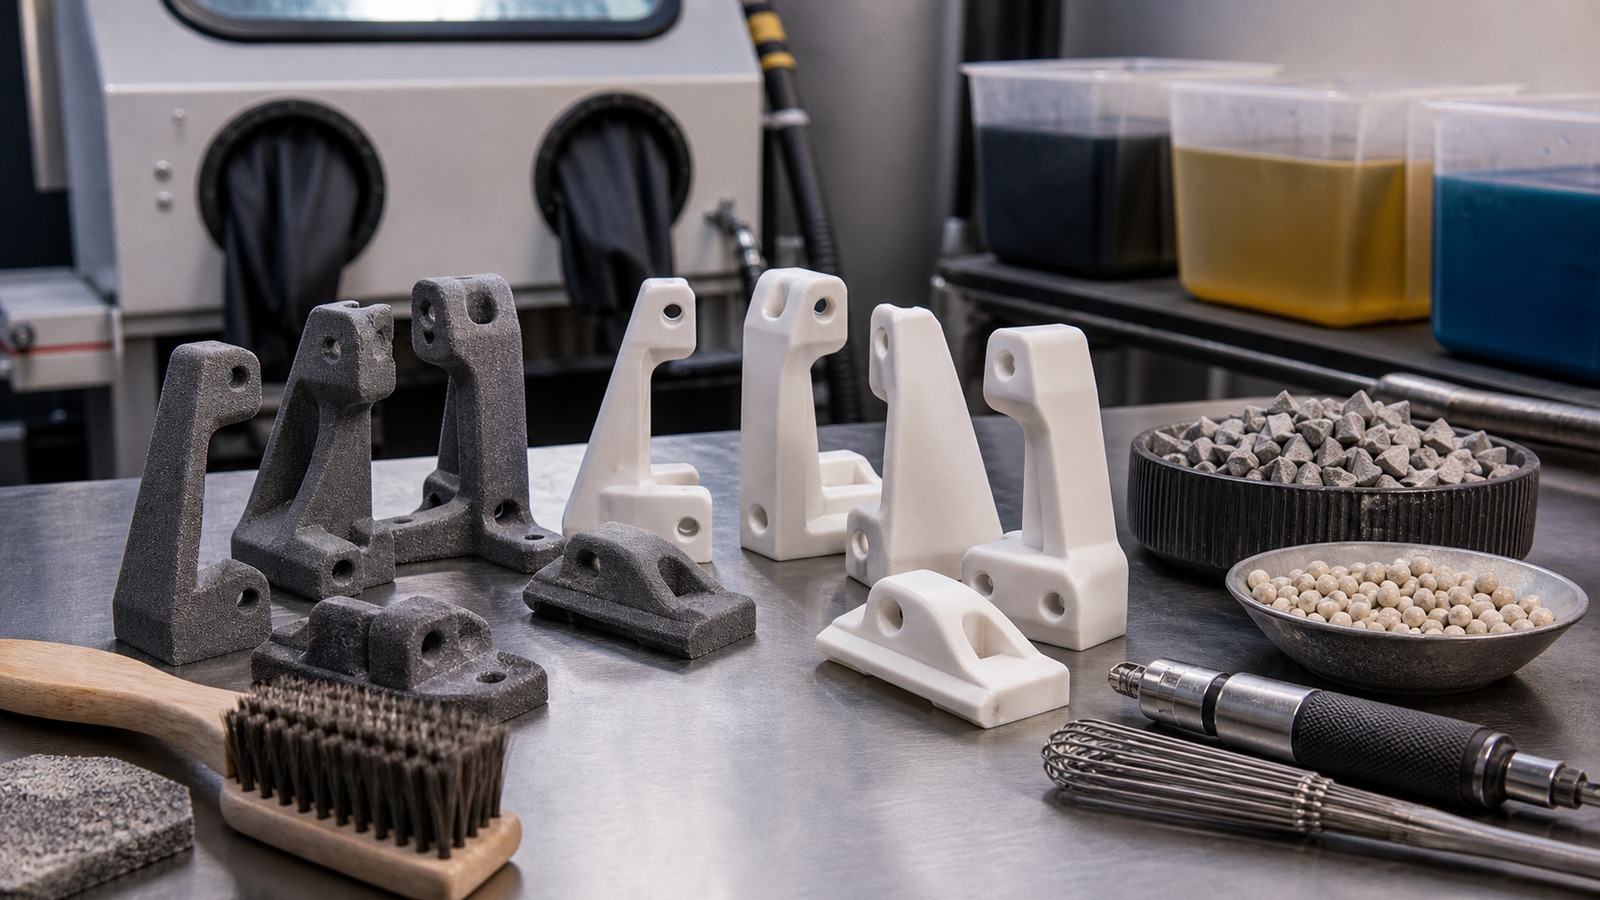
Labor also matters. Depowdering, blasting, dyeing, sorting, inspection, and packing can take longer than expected, especially for intricate parts with internal cavities or delicate features.
Why Batching Changes the Math
SLS becomes more attractive when many parts share one build. The powder bed can hold nested parts in three dimensions, so a service bureau or business can pack multiple customer jobs or repeated components together. Better packing lowers cost per part.
Batching has limits. Parts need spacing, thermal control, and clean powder removal. Overpacked builds can create heat or cleaning problems. The goal is a stable build with enough density to use machine volume efficiently.
Business Use Cases
Businesses often justify SLS when tooling would be too slow, geometry is too complex for simpler processes, or short production runs need functional nylon parts. Examples include jigs, fixtures, clips, housings, ducts, grippers, orthotics, and small replacement-part runs.
The business case improves when SLS reduces assembly, replaces several components, or avoids support removal. If the part is a plain block, machining or FDM may be cheaper. If the part has complex internal passages or many small repeated features, SLS may win.
Hobbyist Use Cases
Hobbyists usually access SLS through service bureaus rather than owning a machine. That makes it useful for parts that deserve better strength, surface quality, or geometry than home FDM can deliver. Miniature accessories, drone parts, camera mounts, and wearable components can all make sense when the design is worth the higher price.
For casual single prints, SLS may feel expensive because setup, handling, and shipping are baked into the quote. The best hobby use is a finalized design, several parts batched together, or a component where nylon performance matters.
Ways to Lower SLS Cost
Reduce unnecessary solid volume, hollow bulky parts when powder removal is possible, avoid excessive height, combine small parts into logical builds, and choose finish levels intentionally. A raw functional part is cheaper than a dyed, polished, inspected part with tight cosmetic requirements.
Design revisions are another cost lever. A small test order can confirm fit before a larger batch. Paying for one pilot set is usually cheaper than discovering that a hundred parts need a 0.3 mm clearance change.
When SLS Is Worth Paying For
SLS is worth considering when the part needs no support scars, usable nylon strength, complex geometry, small-batch production, or professional finishing. It is less compelling when the part is large, simple, nonfunctional, or needed only as a rough visual model.
A good quote evaluation compares the finished-use part, not just raw printer price. Include design time, support removal, finishing, assembly, defect rate, and delivery time before deciding whether SLS is expensive or efficient.
FAQ
Why is SLS more expensive than FDM?
SLS machines, powder handling, cooldown, depowdering, finishing, and quality control add cost, especially for one-off parts.
How can I reduce SLS printing cost?
Lower volume, reduce build height, batch parts, simplify finishing, and test critical fits before ordering a larger run.
Is SLS affordable for hobbyists?
It can be affordable through service bureaus when the part benefits from nylon strength or complex geometry, but FDM is cheaper for simple prints.