The Material Choice Controls the Result
SLS material selection is mostly about matching the part’s job to the powder’s mechanical behavior. Nylon 12, nylon 11, filled nylons, flexible TPU powders, and specialty polymers can all be useful, but they do not behave the same in impact, heat, stiffness, surface finish, or long-term use.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose stringing, warping, weak layers, clogs, and moisture bubbles before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful support removal, sanding, painting, smoothing, and part testing.
A: It is most useful for makers matching material behavior to the job instead of only the color.
The Material Choice Controls the Result
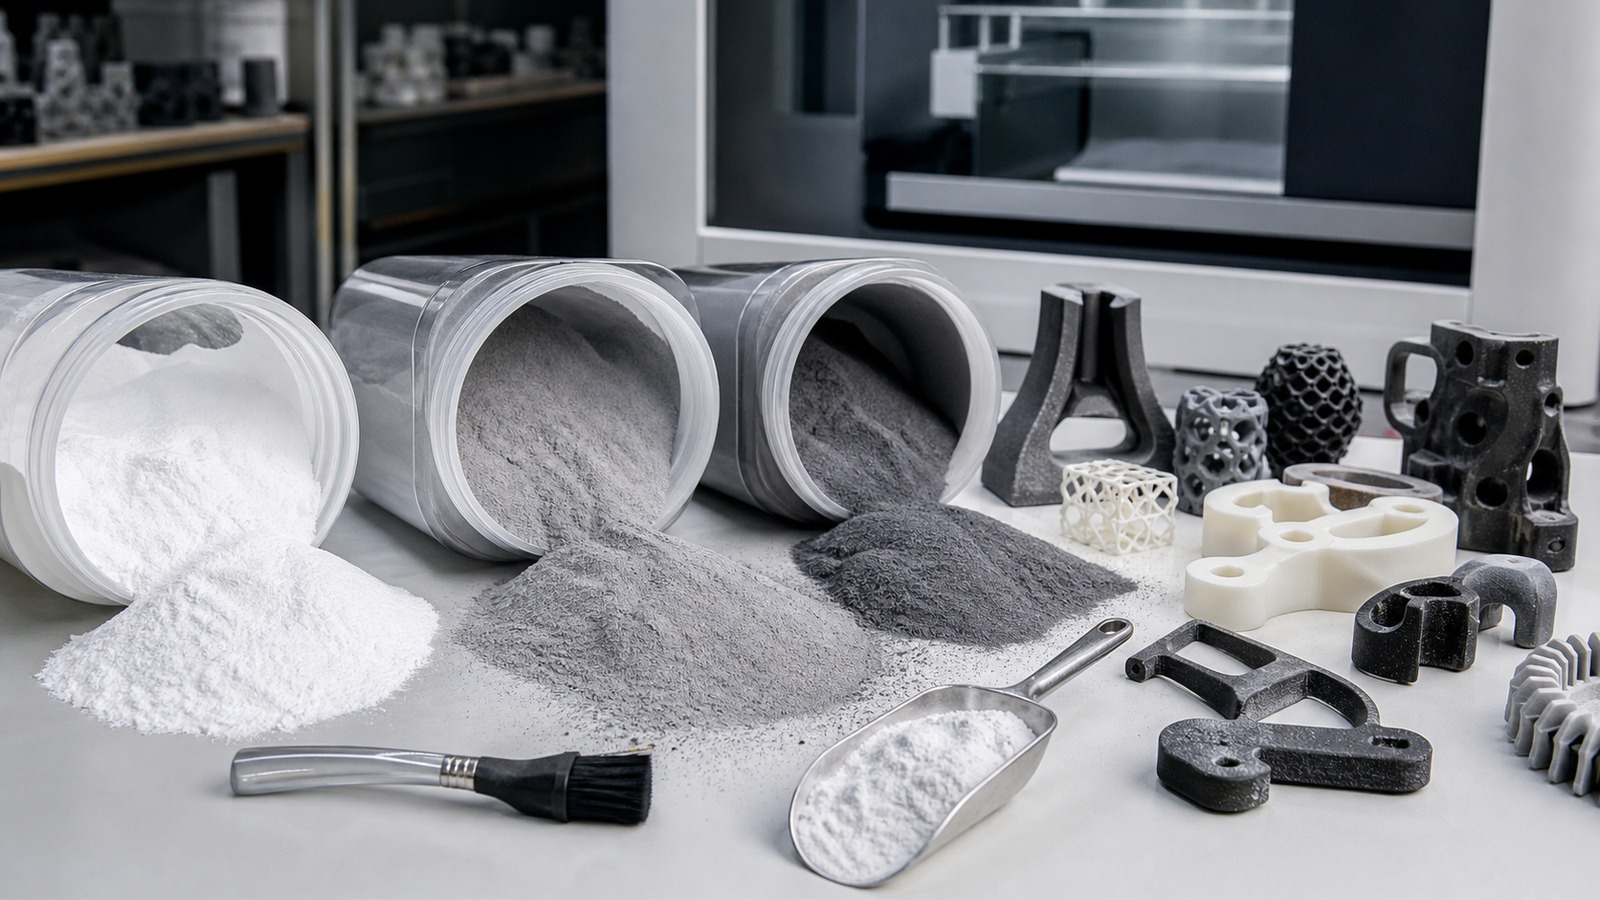
SLS material selection is mostly about matching the part’s job to the powder’s mechanical behavior. Nylon 12, nylon 11, filled nylons, flexible TPU powders, and specialty polymers can all be useful, but they do not behave the same in impact, heat, stiffness, surface finish, or long-term use.
Unlike filament printing, SLS material choice also affects powder reuse, refresh rate, depowdering, dyeing, and surface texture. A material that prints well can still be the wrong choice if it is too stiff, too flexible, too costly, or too difficult to finish for the application.
PA12: The General-Purpose SLS Workhorse
PA12 is the most familiar polymer SLS material because it balances strength, dimensional stability, toughness, surface finish, and cost. It is often used for prototypes, housings, brackets, clips, ducting, fixtures, and small production parts.
Choose PA12 when the part needs dependable nylon behavior without extreme flexibility or heat requirements. It is a sensible default for many functional parts, especially when the design is already proven and the priority is consistent output.
PA11: Better Ductility and Impact Behavior
PA11 is often selected when a part needs more ductility and impact resistance than PA12. It can be useful for hinges, snap features, wearable parts, sports components, and designs that flex or absorb impact rather than simply holding shape.
PA11 is not automatically better than PA12. It may cost more and the exact properties depend on the supplier, machine, and process. The key question is whether the added ductility solves a real part problem.
Glass-Filled and Mineral-Filled Nylon
Filled nylon powders add stiffness, heat resistance, or dimensional stability. Glass-filled PA12 can work well for fixtures, housings, tooling aids, and parts that need a more rigid feel. Filled materials can also be more abrasive and may be less forgiving in thin flexible features.
Use filled powders when stiffness and thermal behavior matter more than flex. Avoid them for living hinges, delicate snap fits, or parts that need high elongation unless the material data supports the design.
TPU and Flexible SLS Materials
Flexible SLS powders such as TPU open the door to gaskets, grips, padding, footwear concepts, protective parts, and soft-touch components. They allow geometry that would be difficult to mold in low volume and can avoid the stringing and path limitations of flexible filament printing.
The tradeoff is accuracy, surface texture, and cleanup. Flexible powder parts may need more careful depowdering and validation. Designers must think about wall thickness, rebound, compression, and how the part will be cleaned after printing.
Color, Finish, and Post-Processing
Most polymer SLS parts come out white, gray, or natural depending on the powder and machine. Dyeing is common for black or colored production parts. Bead blasting and tumbling can smooth the powdery texture, while sealing or coating can improve feel or appearance.
Post-processing can change tolerances. A dyed, tumbled, or sealed part may fit differently than a raw part. Critical dimensions should be checked after the chosen finish, not only after depowdering.
How to Pick an SLS Material
Start with the part’s failure mode. If it may snap, evaluate ductility. If it may deform under heat, check thermal properties. If it needs a rigid fixture feel, compare stiffness. If it touches skin or fluid, check supplier documentation and application suitability.
Then compare cost and availability. PA12 is often easiest to source broadly, while specialty powders may require a specific service bureau or machine ecosystem. A strong material choice is one that performs well and fits the production workflow.
FAQ
What is the best material for SLS printing?
PA12 is the most common all-around choice, while PA11 is better for ductility and impact-focused parts.
Can SLS make flexible parts?
Yes. Flexible powders such as TPU can produce soft or elastic components, though cleanup and tolerances need extra attention.
Can SLS parts be colored?
Yes. Many nylon SLS parts can be dyed or finished after printing, but finishing can affect fit and surface feel.