Why Industry Uses SLS
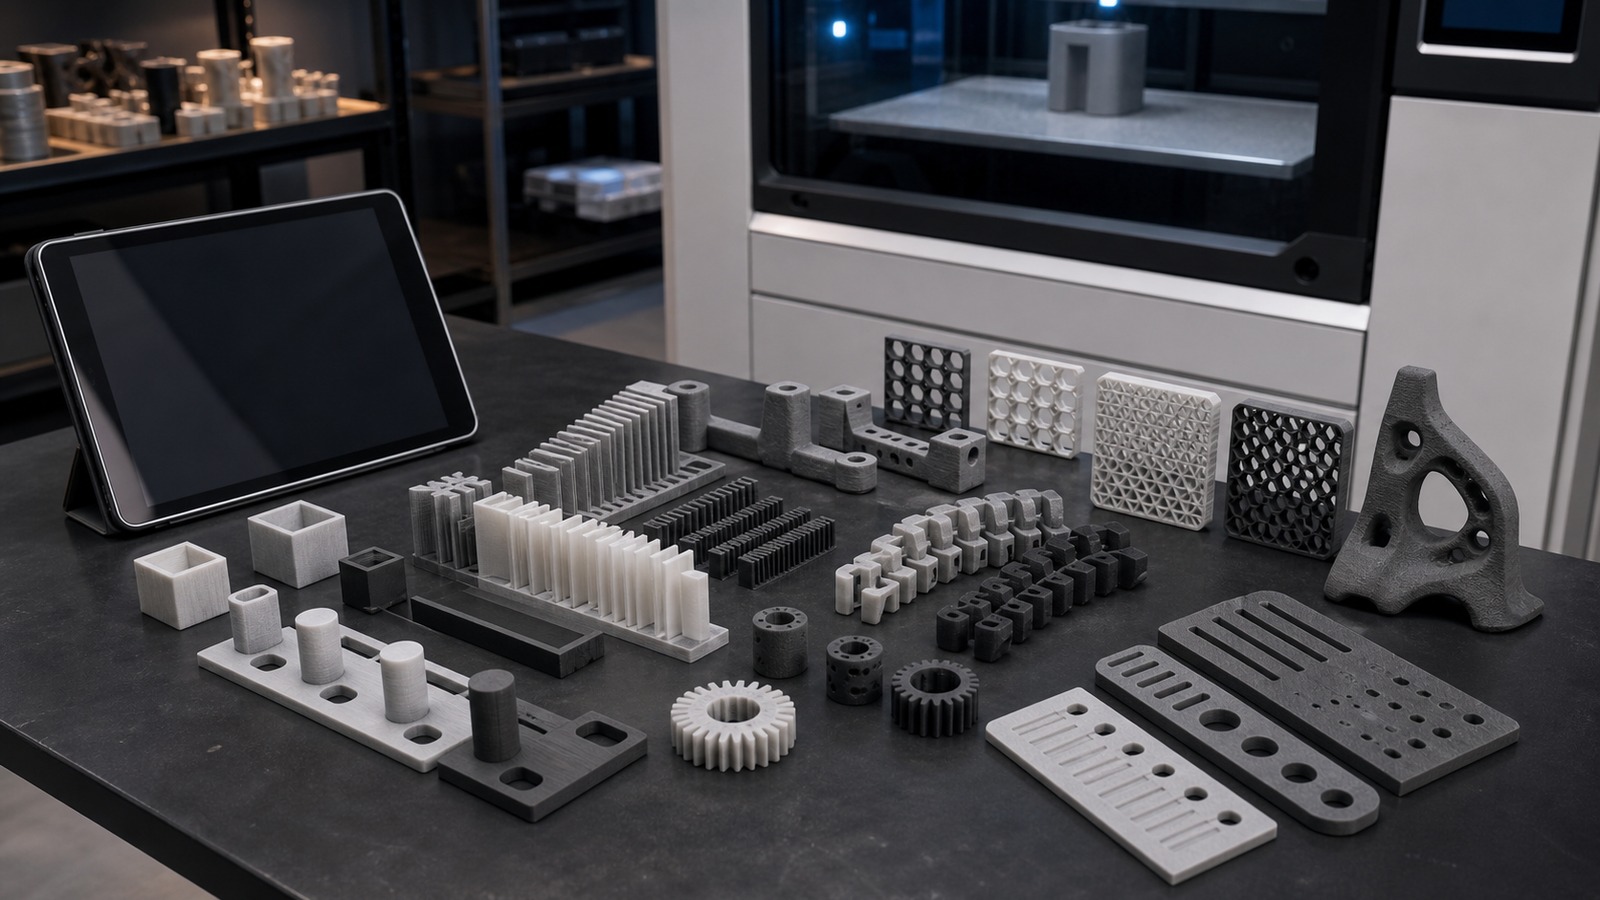
Selective laser sintering is valuable in industry because it produces functional polymer parts without dedicated tooling and without conventional support structures. That combination fits prototypes, bridge production, replacement parts, tooling aids, and complex small-batch components.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose slow throughput, inconsistent tolerances, weak parts, and unclear requirements before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful inspection, part testing, finishing, assembly, and revision control.
A: It is most useful for teams using 3D printing as a workflow tool, not only a hobby machine.
Why Industry Uses SLS
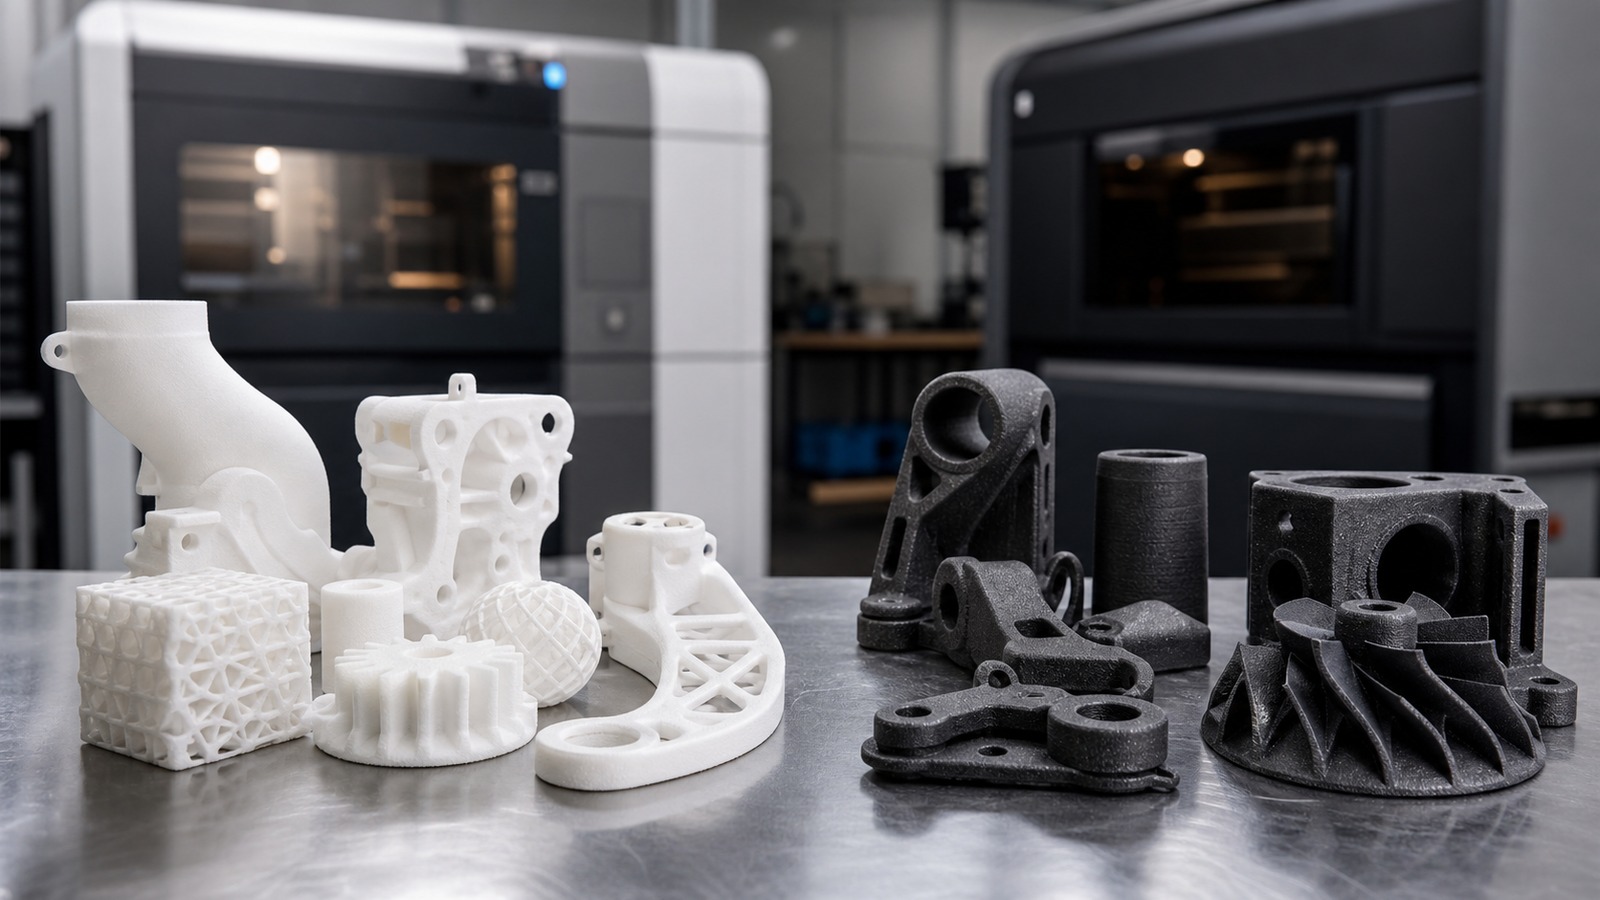
Selective laser sintering is valuable in industry because it produces functional polymer parts without dedicated tooling and without conventional support structures. That combination fits prototypes, bridge production, replacement parts, tooling aids, and complex small-batch components.
The process is especially useful when a part needs nylon toughness, internal features, low-volume customization, or many pieces packed into one build. It is less useful when the job requires very smooth cosmetic surfaces straight out of the printer or very high-volume commodity production.
Product Development and Prototyping
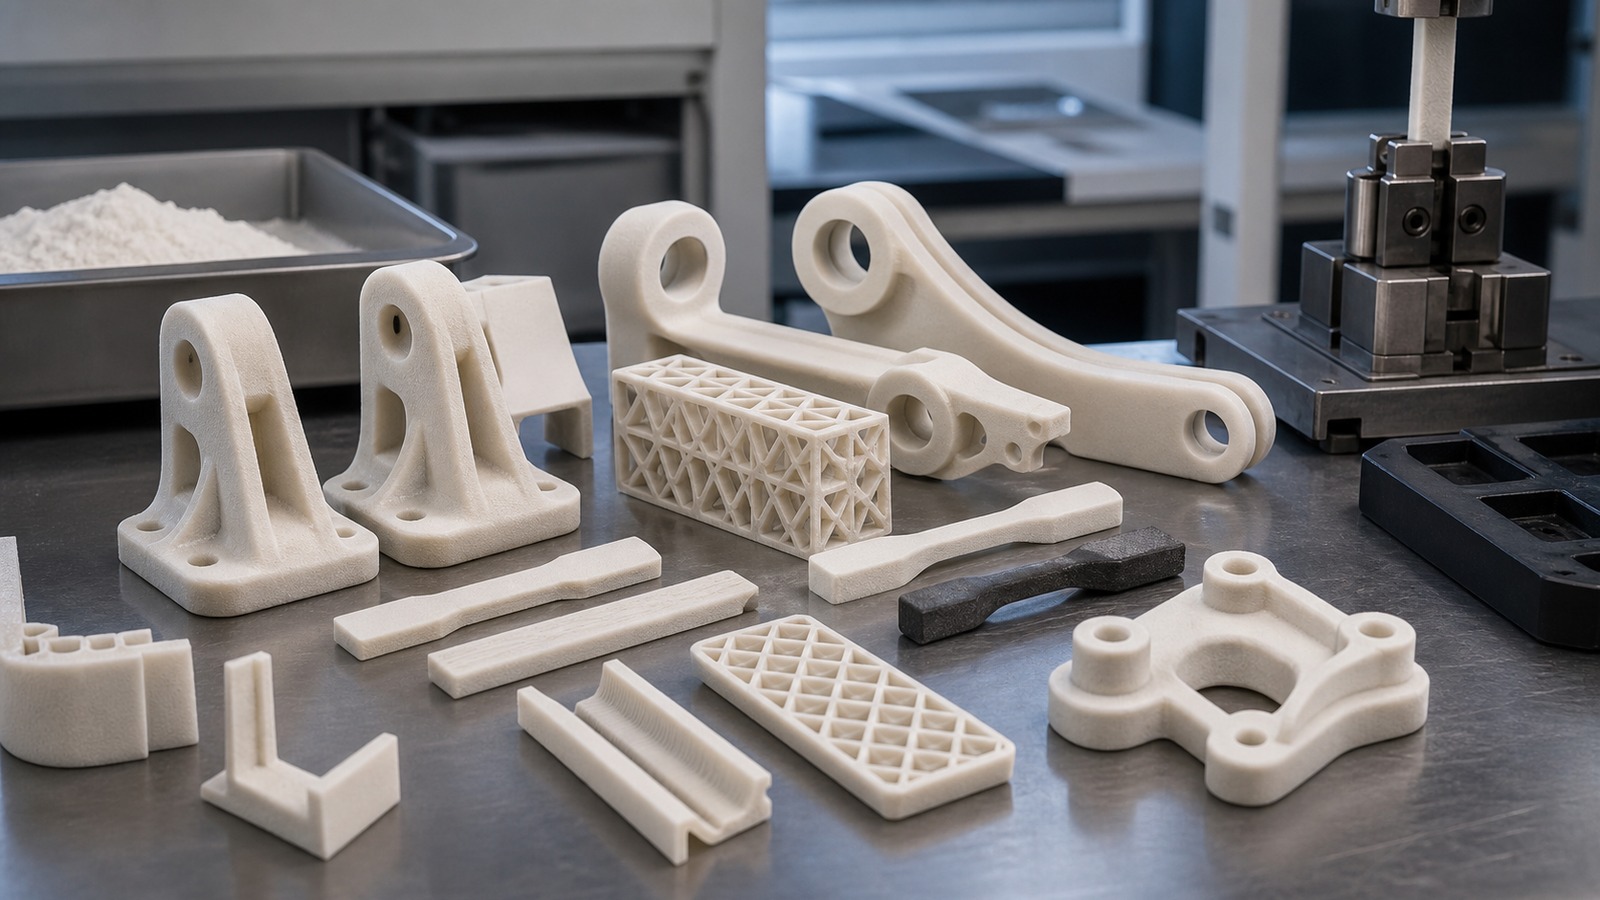
Engineering teams use SLS to test housings, clips, hinges, ducts, and assemblies before tooling. The parts can be strong enough for handling, fit checks, ergonomic trials, and limited functional testing. That makes SLS more informative than a fragile visual model in many product-development cycles.
Because support removal is minimal, designers can prototype shapes with undercuts, internal passages, and complex contours. Iteration is faster when the prototype resembles the intended manufacturing geometry rather than a simplified print-only version.
Jigs, Fixtures, and Manufacturing Aids
Factories use SLS for fixtures, grippers, nests, drill guides, inspection gauges, and assembly aids. These parts often have custom geometry that fits one product or workstation, so traditional tooling can be too slow or expensive.
Nylon SLS fixtures can be lightweight, durable, and easy to revise. A production team can test an ergonomic improvement, update the file, and order a new version without waiting for machined tooling unless the load or tolerance demands it.
Medical, Dental, and Wearable Applications
SLS can support medical models, orthotic concepts, prosthetic components, surgical planning aids, and wearable devices when material and regulatory requirements are addressed. The process is appealing because it can make complex custom geometry from digital patient or product data.
These uses require disciplined validation. Biocompatibility, cleaning, traceability, and regulatory requirements depend on the exact application and material. SLS is a manufacturing route, not automatic approval for medical use.
Automotive and Aerospace Support
Automotive teams use SLS for prototype housings, ducts, brackets, interior concepts, clips, and tooling. Aerospace teams can use polymer powder bed parts for prototypes, fixtures, ducting concepts, and non-flight or qualified applications where the material and process meet requirements.
The advantage is iteration and geometric freedom. Lightweight shapes, complex routing, and integrated features can be evaluated quickly. For production or flight hardware, the value must be matched by inspection and qualification.
Small-Batch and Bridge Production
SLS is often used between prototype and tooling. A company may need 50, 500, or 2,000 parts before injection molding is ready or before demand is proven. SLS can fill that gap without the tooling delay.
It can also serve as the final process for low-volume products. Custom orthotics, specialty equipment parts, robotics brackets, and niche consumer products may never reach molding quantities. In those cases, additive manufacturing can be the production method rather than a temporary step.
Industrial Limits
SLS parts still need design rules, process control, powder management, cooling, depowdering, finishing, and inspection. Surface texture, dimensional tolerance, powder escape, and material aging all matter. Industrial users succeed by treating SLS as a controlled process, not a push-button shortcut.
The strongest applications begin with a real reason to use the process: complex geometry, low volume, customization, part consolidation, weight savings, or shortened lead time. Without one of those advantages, another process may be better.
FAQ
What industries use SLS printing?
Product development, manufacturing, medical, dental, automotive, aerospace, robotics, consumer products, and service bureaus all use SLS where functional polymer parts make sense.
Can SLS be used for production?
Yes. It is common for bridge production and low-volume final-use parts when material, tolerance, finish, and economics fit the job.
Why choose SLS over FDM for industrial parts?
SLS offers stronger design freedom, no conventional support scars, good nylon materials, and efficient batch production for complex shapes.