The Main Advantage Is Functional Freedom
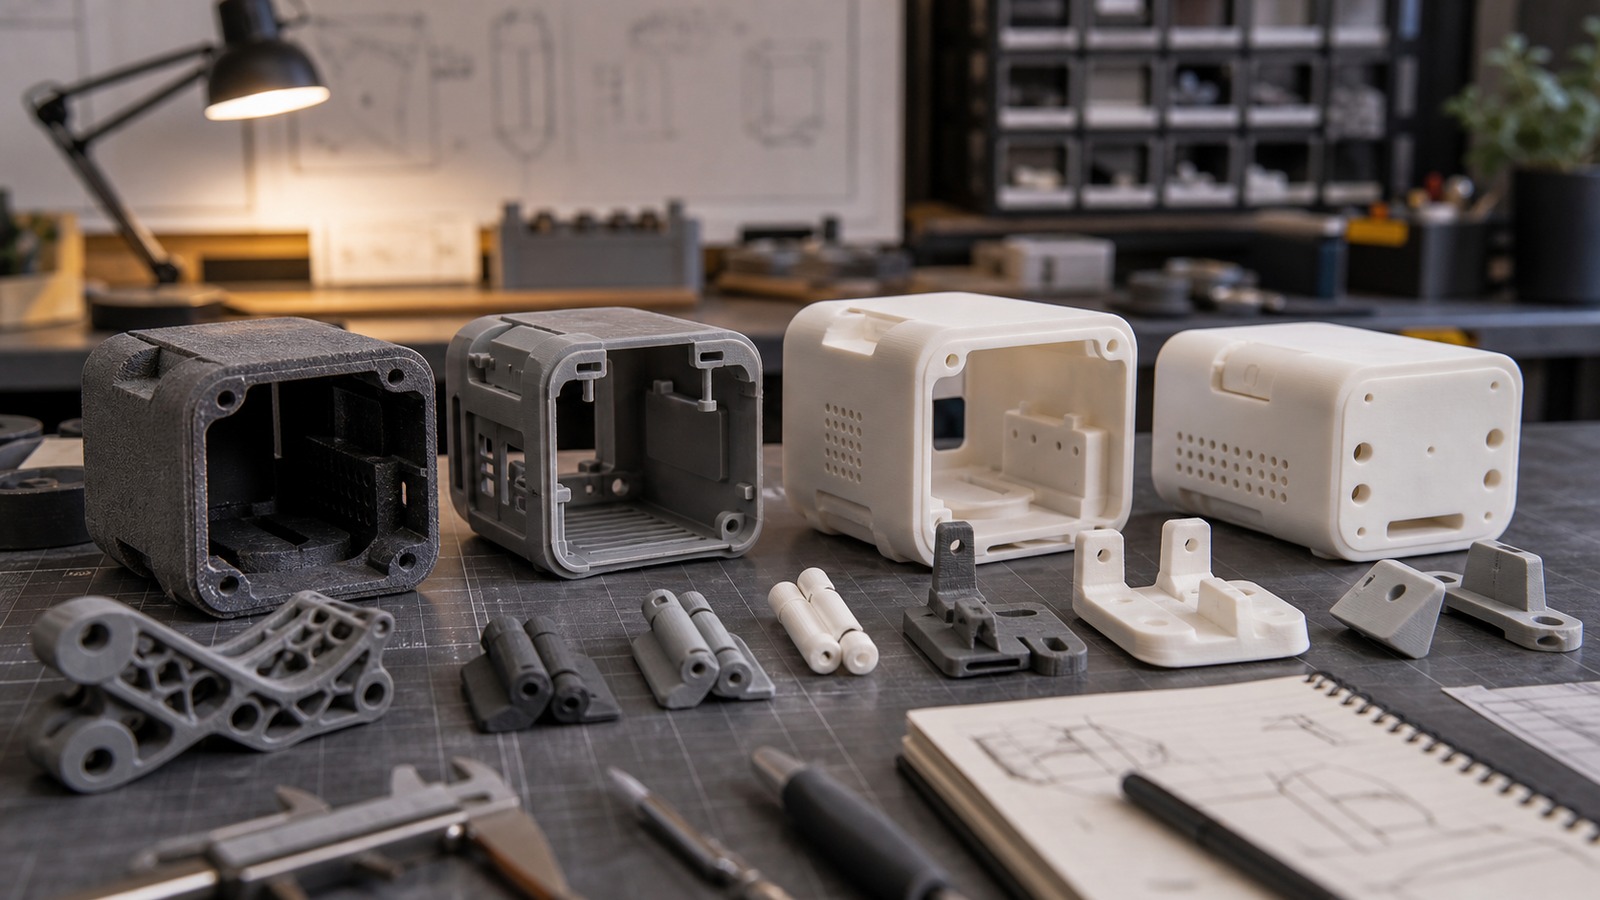
SLS is useful for functional parts because it combines nylon materials, complex geometry, and support-free building inside a powder bed. The process can make clips, housings, ducts, fixtures, brackets, hinges, and nested batches with fewer design compromises than many support-heavy methods.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose thin walls, unsupported features, tight fits, bad meshes, and weak load paths before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful test fits, inserts, sanding, assembly, and revision notes.
A: It is most useful for makers designing parts that need to fit, move, or survive use.
The Main Advantage Is Functional Freedom
SLS is useful for functional parts because it combines nylon materials, complex geometry, and support-free building inside a powder bed. The process can make clips, housings, ducts, fixtures, brackets, hinges, and nested batches with fewer design compromises than many support-heavy methods.
That does not mean SLS is always better. It means SLS solves a specific set of problems: parts that need toughness, complexity, low-volume production, and clean geometry without manually removed support towers.
No Traditional Support Structures
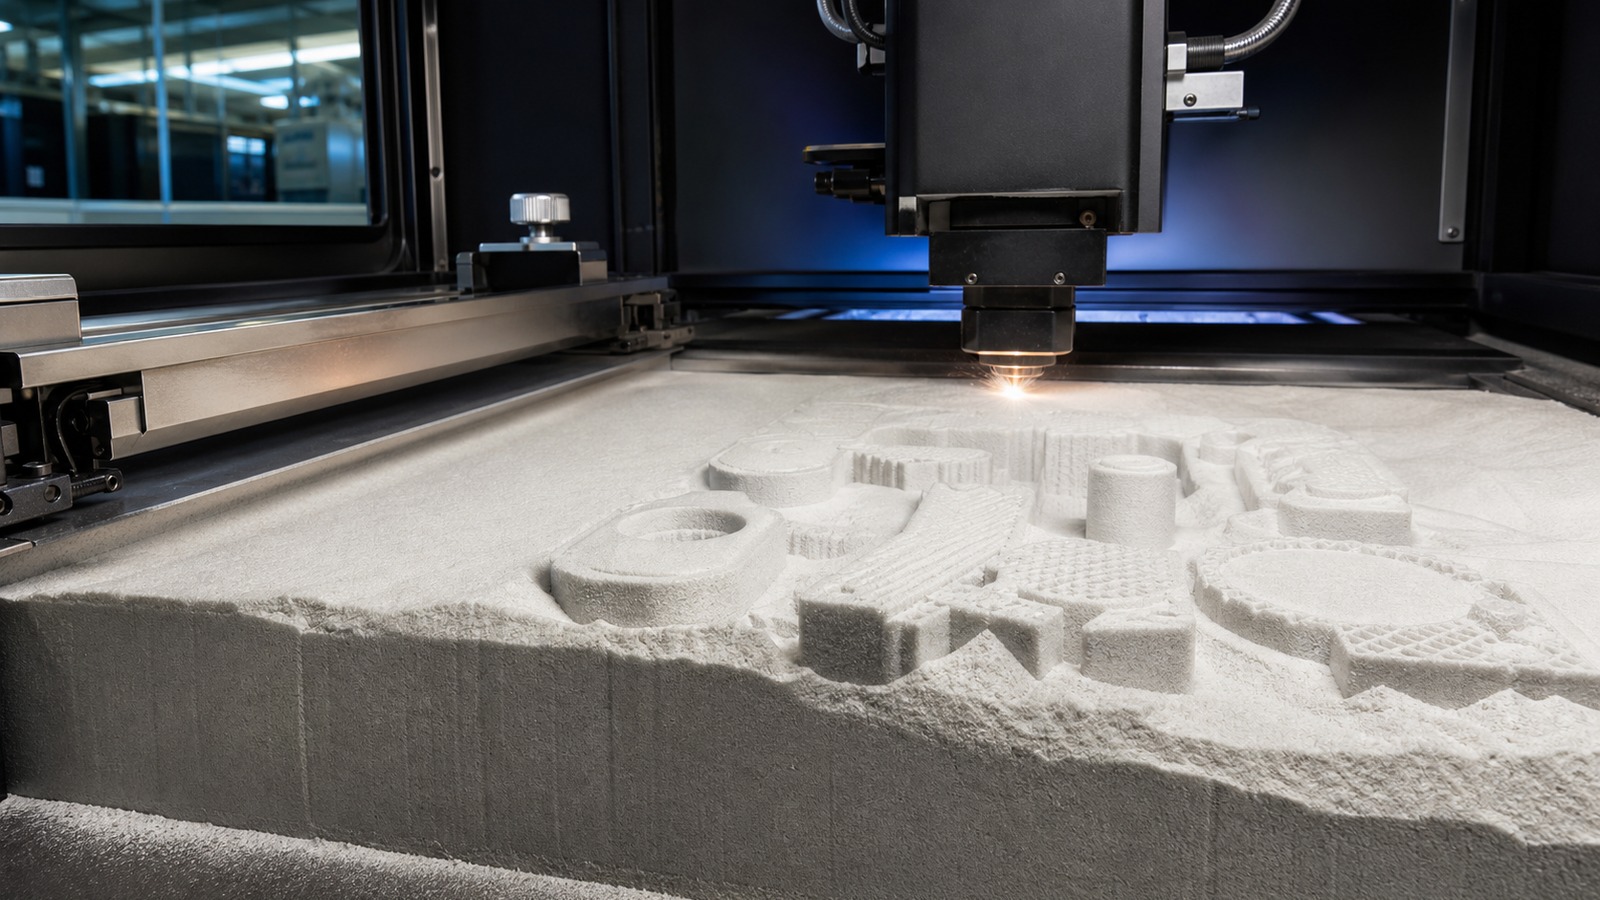
The unfused powder supports each layer as the print grows. This allows overhangs, internal shapes, lattices, and interlocking assemblies that would be difficult on FDM or resin printers. It also avoids scars from clipped support structures on important surfaces.
Support-free printing changes how designers think. Instead of asking where support marks can be hidden, the designer can focus on powder escape, wall thickness, packing, and whether the part can be cleaned properly after printing.
Good Strength for Nylon Parts
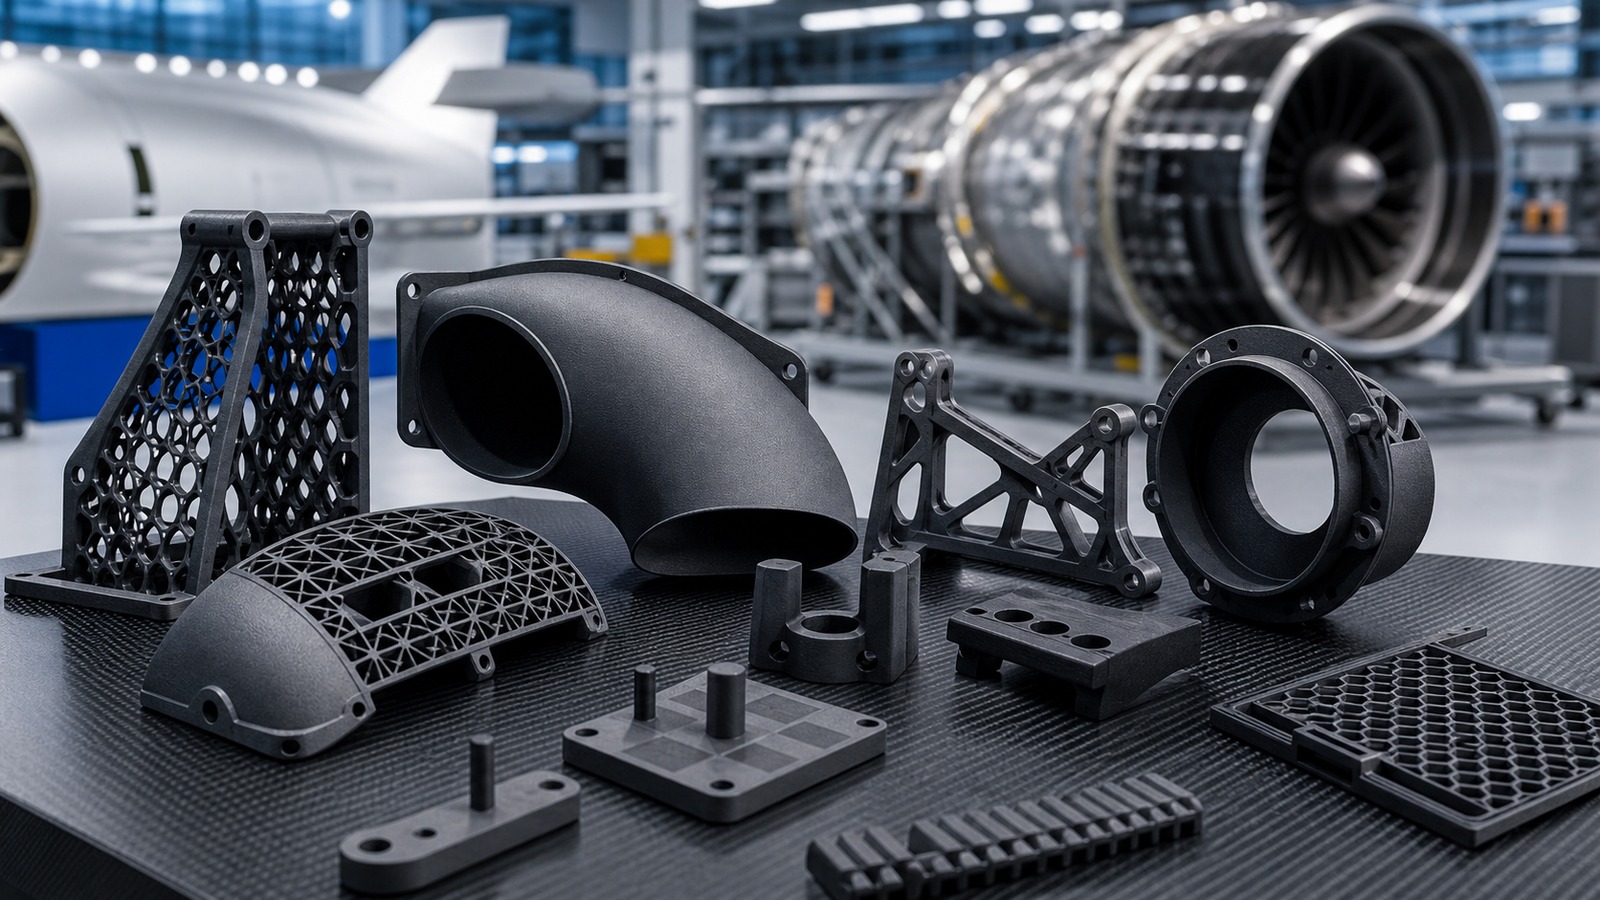
Polymer SLS parts are often made from nylon powders such as PA12 or PA11. These materials can produce tough functional parts suitable for prototypes, fixtures, enclosures, clips, and low-volume products. The lack of filament road gaps can also make SLS parts feel more uniform than many FDM parts.
Strength still depends on material, wall thickness, geometry, machine settings, and finishing. A poorly designed SLS part can fail. The advantage is that the process starts with a strong functional material family and fewer orientation penalties than typical FDM printing.
Efficient Batch Production
SLS can pack many parts in one build volume because pieces can be nested throughout the powder bed. That makes it attractive for service bureaus, product teams, and small manufacturers running many small or medium parts at once.
Batching spreads setup, heating, cooling, and handling across more parts. The result can be a competitive cost per part when geometry is complex or quantities are too low for tooling.
Design Freedom for Complex Parts
Internal channels, duct-like shapes, lattice structures, organic forms, and consolidated assemblies are all strong SLS candidates. The process can create geometry that would be awkward to machine and difficult to support in other printing processes.
This is where SLS often beats a simple cost comparison. If a single printed part replaces several assembled parts, reduces fasteners, or enables a lighter shape, the manufacturing value is not just the print price.
Fast Iteration Without Tooling
SLS lets teams move from CAD to usable nylon parts without injection molds or custom tooling. That supports prototype testing, pilot runs, bridge production, and product revisions. A design can be updated after physical testing and printed again without changing a mold.
The process is especially valuable before demand is certain. A business can test a product or support spare parts without committing to high tooling costs too early.
The Limits Behind the Advantages
SLS surfaces are often grainy, colors may require dyeing, trapped powder needs escape paths, and cooldown adds time. Very large solid parts can be expensive and thermally challenging. Fine cosmetic surfaces may need post-processing.
The best SLS parts are designed for SLS. Wall thickness, hole size, drainage, packing, and finish all affect the result. When those details are handled well, SLS becomes one of the most practical additive methods for functional polymer parts.
FAQ
What is the biggest advantage of SLS 3D printing?
The biggest advantage is producing complex functional nylon parts without conventional support structures.
Are SLS parts stronger than FDM parts?
Often, but not always. SLS nylon parts can be very functional, while FDM strength depends heavily on orientation, material, walls, and layer bonding.
Why is SLS good for small-batch production?
Many parts can be nested in one powder bed, spreading setup and handling across the batch without injection molding tooling.