Why SLS Problems Happen
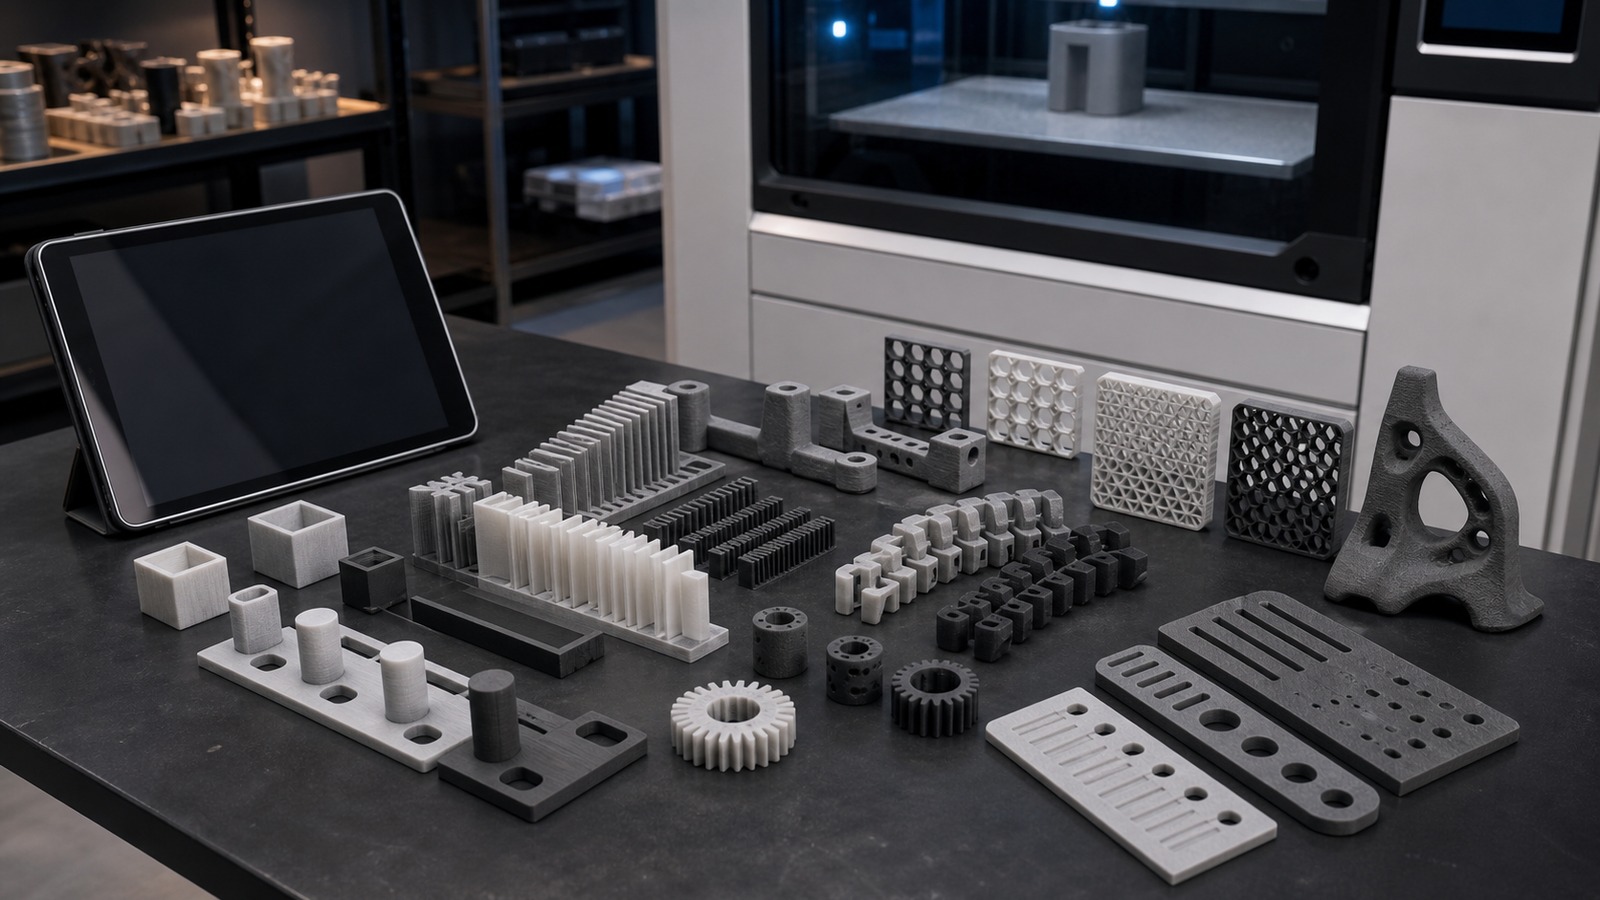
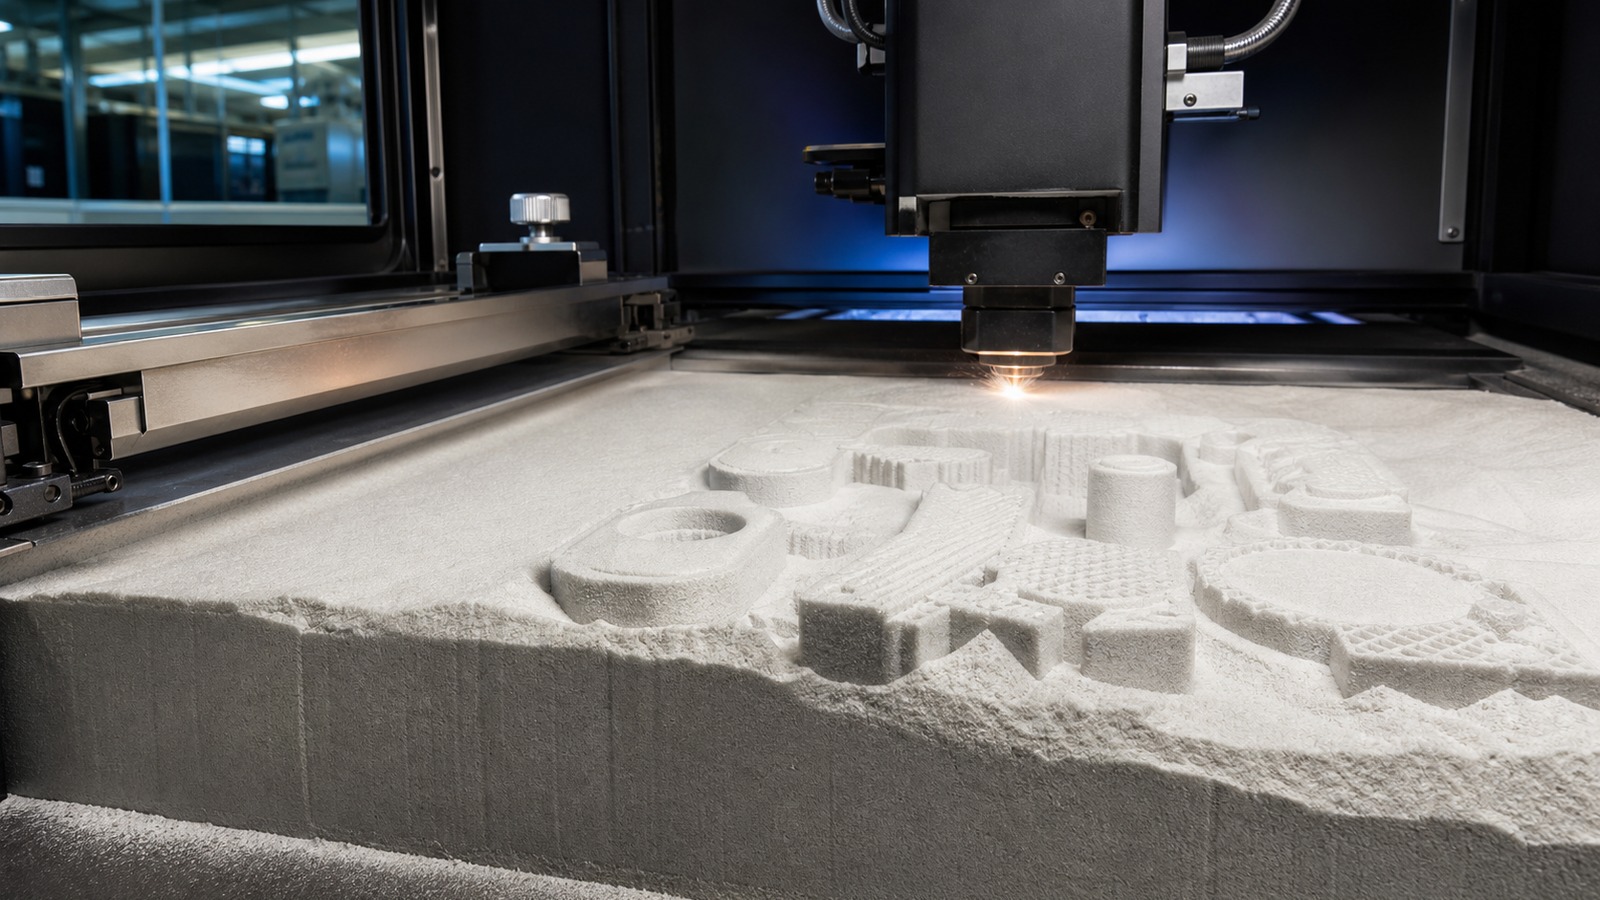
Selective laser sintering is more forgiving than support-heavy printing processes, but it is not failure-proof. Most SLS problems come from powder condition, heat control, packing density, wall thickness, part geometry, cooldown, or depowdering. The part may look fine in CAD and still warp, curl, trap powder, or lose detail if the process window is poor.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose poor first layers, weak parts, stringing, warping, and rough surfaces before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful support removal, sanding, painting, fitting, and practical testing.
A: It is most useful for makers who want cleaner prints and fewer wasted attempts.
Why SLS Problems Happen
Selective laser sintering is more forgiving than support-heavy printing processes, but it is not failure-proof. Most SLS problems come from powder condition, heat control, packing density, wall thickness, part geometry, cooldown, or depowdering. The part may look fine in CAD and still warp, curl, trap powder, or lose detail if the process window is poor.
Troubleshooting works best when the defect is separated from the whole build. A curled edge, rough surface, weak thin wall, clogged channel, or dimensionally tight hole each points to a different cause. SLS quality comes from matching design rules to material and machine behavior.
Warping and Curling
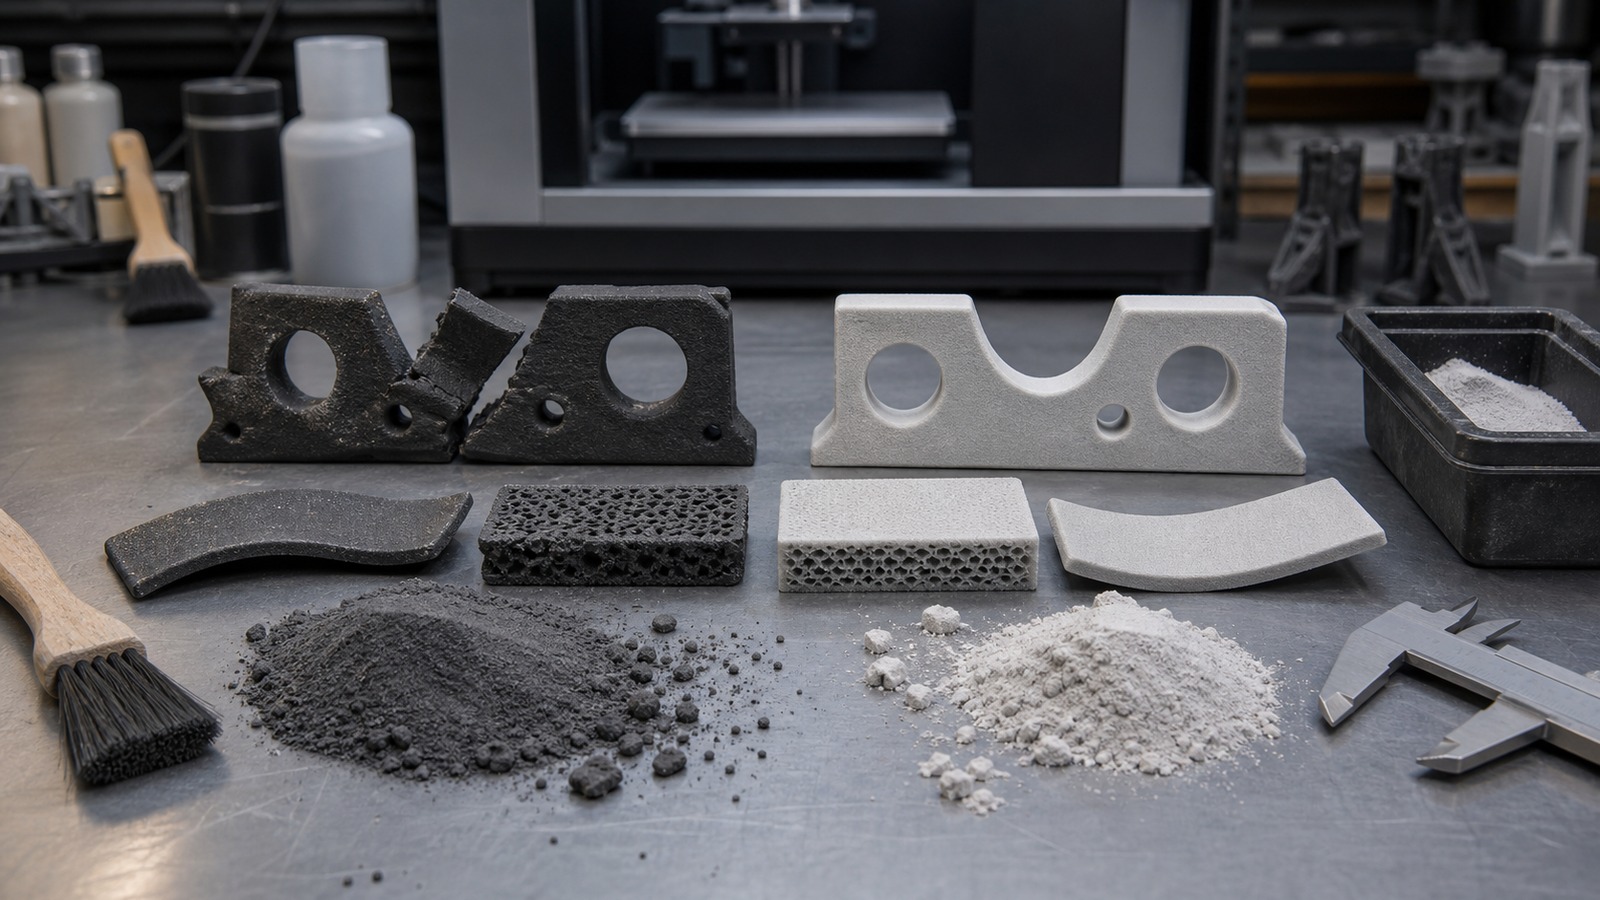
Warping happens when thermal stress pulls a part out of shape as powder heats and cools. Large flat plates, uneven wall thickness, sharp transitions, and aggressive packing can make the problem worse. Removing parts before the powder cake cools enough can also create distortion.
Reduce warping with more even wall sections, generous radii, better orientation, smaller broad flats, and adequate cooldown. If a functional plate must stay flat, consider ribs, breaks in the surface, or machining a critical face after printing.
Poor Detail or Soft Edges
Soft edges can come from overheated powder, old powder blend, geometry below the machine’s practical detail limit, or finishing that rounds features too aggressively. Small text, thin fins, and tiny holes are common trouble spots.
Increase feature size, use raised details that can survive depowdering, and verify the service bureau’s minimum wall and detail guidance. A detail that looks clear on screen may disappear after blasting or dyeing.
Powder Trapped Inside the Part
Hollow SLS parts need escape paths for unfused powder. Long blind channels, sealed cavities, and small drain holes can trap material and add weight. Trapped powder may also affect balance, rattle, or later cleaning.
Design access holes large enough for the powder and cleaning method. For complex ducts or housings, confirm the cleaning plan before ordering the part. If powder cannot be removed, the design may need to be split.
Weak Thin Features
Thin walls, pins, snap features, and clips can break during depowdering or service. Nylon is tough, but it still needs enough section thickness for the load and cleaning process. Sharp roots create stress concentration.
Add fillets at transitions, thicken loaded features, avoid long unsupported thin fins, and choose PA11 or another ductile material when impact or flex is the main risk. Test clips and hinges before ordering a large batch.
Dimensional Fit Problems
SLS parts can be accurate, but holes, slots, snap fits, and mating surfaces still need clearance. Surface texture, shrinkage compensation, material, orientation, and post-processing all affect fit. A dyed or tumbled part may not match the raw measurement exactly.
Use tolerance coupons for critical assemblies and leave practical clearance for moving parts. For tight mechanical interfaces, machine critical surfaces or add inserts rather than relying on raw printed geometry alone.
A Practical Fixing Order
Begin with the defect location: edge, thin feature, hole, surface, cavity, or whole part. Then check geometry, material, orientation, packing, and finishing. If only one feature fails, print or order a small test version of that feature before changing the entire model.
For production, keep records of powder type, finish, part orientation, and supplier. SLS problems become much easier to solve when each build has a traceable process history instead of only a finished part photo.
FAQ
Why do SLS parts warp?
Warping usually comes from thermal stress, broad flat geometry, uneven walls, poor cooldown, or material/process issues.
How do I prevent trapped powder in SLS prints?
Add accessible powder escape holes, avoid blind cavities, and split complex designs when cleaning paths are too narrow.
Why are small details missing on my SLS part?
Small details may be below the process limit or may be softened by powder condition, heat, blasting, dyeing, or tumbling.