The Main Difference
EBM and SLM are both metal powder bed fusion processes, but EBM uses an electron beam in a vacuum while SLM uses a laser, typically in an inert gas environment. Both melt metal powder into dense parts layer by layer.
A: Match the model, material, settings, and finish plan to the purpose of the print.
A: Bed leveling, surface cleanliness, nozzle height, temperature, and material condition are the usual suspects.
A: No. Slower speeds can improve detail, but heat buildup and profile balance still matter.
A: Use the right material, more walls, smart orientation, enough infill, and realistic load testing.
A: Temperature, retraction, travel moves, moisture, and material type all contribute.
A: Diagnose poor first layers, weak parts, stringing, warping, and rough surfaces before buying parts.
A: Very important; it shows toolpaths, supports, layer changes, and possible weak spots before printing.
A: First layers, simple calibration prints, support cleanup, and basic material profiles.
A: Clean orientation, tuned settings, good material handling, and careful support removal, sanding, painting, fitting, and practical testing.
A: It is most useful for makers who want cleaner prints and fewer wasted attempts.
The Main Difference
EBM and SLM are both metal powder bed fusion processes, but EBM uses an electron beam in a vacuum while SLM uses a laser, typically in an inert gas environment. Both melt metal powder into dense parts layer by layer.
The process choice affects material compatibility, thermal behavior, surface finish, supports, productivity, and machine requirements.
How EBM Behaves
EBM operates at high build temperatures and can reduce residual stress for certain alloys. It can also enable stacking strategies in the powder bed, which can improve build-envelope use for some production cases.
EBM is closely associated with titanium and medical or aerospace components, though the exact fit depends on equipment and qualification.
How SLM Behaves
Selective Laser Melting, also called laser powder bed fusion in many standards contexts, uses a laser to melt metal powder. It is widely used across stainless steels, aluminum alloys, nickel alloys, titanium, tool steels, and other materials depending on system and powder.
SLM often provides finer surface/detail potential but may require careful support, stress relief, heat treatment, and post-machining.
Material and Part Tradeoffs
Choose EBM when vacuum processing, high-temperature powder bed behavior, titanium production, or stacking fits the application. Choose SLM when laser powder bed material availability, finer features, or supplier access makes more sense.
For critical metal parts, the choice is based on qualified material data and testing, not only process descriptions.
Inspection and Post-Processing
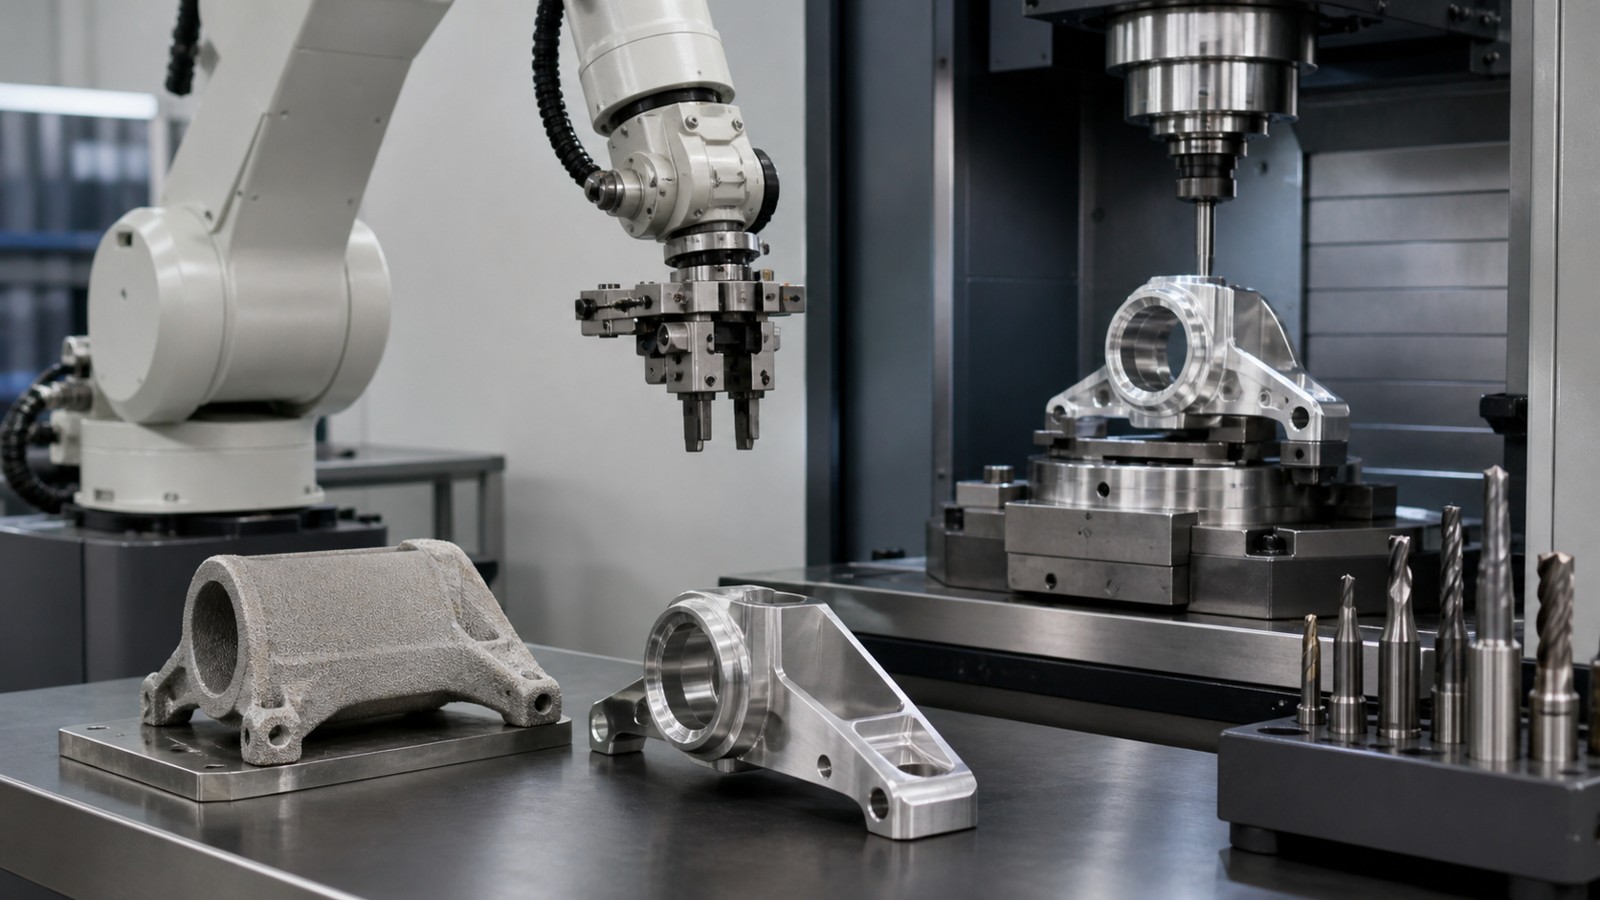
Both processes often need support removal, heat treatment, machining, surface finishing, and nondestructive inspection. Internal porosity, lack-of-fusion defects, surface roughness, and fatigue behavior all matter for high-value parts.
A finished metal additive part is the result of the complete chain: powder, machine, build, heat treatment, machining, and inspection.
FAQ
Is EBM stronger than SLM?
Not automatically. Strength depends on alloy, process parameters, heat treatment, geometry, defects, and inspection.
Which process is better for titanium?
Both can process titanium alloys, but EBM is especially associated with high-temperature vacuum titanium workflows.
Do EBM and SLM parts need machining?
Often yes, especially for critical dimensions, sealing faces, and surface finish requirements.